What are the material and certification requirements for exporting food processing machinery?
The core material and certification requirements for exporting food processing machinery are that food-contact surfaces must use stainless steel that complies with the regulations of the destination country, typically grade 304 or 316. Depending on the target market, you must also prepare CE Machinery Directive documentation, food-contact material declarations, hygienic design documentation, and complete traceability records. When evaluating suppliers, buyers should first confirm the specific regulations of the destination country regarding materials, surface finish, and hygienic design, then verify the supporting documents the manufacturer can provide, and only then move on to detailed discussions of plant planning and turnkey projects. Choosing the wrong material or missing documentation are the most common causes of rejection and delay in export projects.
What basic certifications and documents are required for exporting food processing machinery?
The most commonly requested documents for exporting food processing machinery are the CE Machinery Directive Declaration of Conformity (DoC) and the Food Contact Materials (FCM) Declaration, which are the basic entry requirements for the EU market. In Southeast Asian markets such as Thailand, although the regulatory framework differs, buyers typically still require CE documentation as a quality endorsement, along with a Mill Certificate indicating the stainless steel grade and chemical composition. For plant planning and turnkey projects, electrical diagrams, layout drawings, and maintenance manuals must also be provided, as these are checked during customs clearance and factory acceptance. Buyers should ask the manufacturer to list the documents they can provide at the quotation stage to avoid discovering missing items after delivery. The specific numbers of material certificates and test reports must be confirmed based on the actual shipment batch and the requirements of the destination country.
Six key points buyers must check when evaluating food machinery suppliers
Food-contact surface material grade
Confirm whether 304 or 316 stainless steel is specified, and require a material certificate indicating the chemical composition to avoid low-cost substitutes such as 201.
Surface roughness and finishing method
Food-contact surfaces should be polished to a Ra value that meets hygiene standards, typically via mechanical or electropolishing. Roughness data must be confirmed based on actual specifications.
CE and machinery safety documentation
Require a Declaration of Conformity, risk assessment, and electrical safety documents, as these are basic requirements for entering the EU and most international markets.
Cleanability and disassembly for hygienic design
Check whether pipe connections, seals, and dead zones are designed to allow CIP cleaning or manual disassembly without dismantling the machine.
Plant planning and turnkey capability
Confirm whether the manufacturer can plan the production line according to the factory dimensions and product specifications, and handle installation, commissioning, and operator training.
Document traceability and after-sales support
Require a spare parts list, operation manual, and maintenance record format, and confirm the response mechanism for local agents or remote support.
How to choose between 304 and 316 stainless steel?
The choice between 304 and 316 stainless steel depends on the pH value, salt content, and cleaning method of the food product. 304 stainless steel is suitable for general egg processing, dough forming, and neutral food environments. It offers lower cost and good machinability, making it a common choice for egg liquid mixing and metering filling equipment, as well as filling machine frames. 316 stainless steel contains molybdenum, which provides stronger resistance to chloride ion corrosion, making it suitable for salty foods, highly acidic products, or production lines that frequently use chlorine-based cleaning agents. Buyers should decide based on their actual product formulation and cleaning procedures. If the product has high salt content or the cleaning frequency is high, 316 is the safer choice. The final material grade decision should be made jointly with the manufacturer based on product characteristics and cleaning conditions, and must be documented in the material certificate.
What is the difference between CE and the regulations of various countries?
The CE mark is a mandatory requirement in the European Union, covering machinery safety, the Low Voltage Directive, and electromagnetic compatibility, but CE is not globally recognized. Thailand and most Southeast Asian countries have their own industrial standards and food safety regulations. While some buyers accept CE documentation as a quality reference, local requirements may still include TIS standards or import permits. The U.S. market, on the other hand, requires compliance with FDA food contact material regulations and OSHA machinery safety requirements, which are entirely different from the CE system. Buyers should first confirm the mandatory regulations of the destination country, then ask whether the manufacturer has relevant experience. The same machine exported to different countries may require different documentation sets and component adjustments, which is a critical point to clarify in the early stages of plant planning. Specific certification items and scope of application should be confirmed based on actual specifications and announcements from the destination country.
What are the surface treatment requirements for food contact surfaces?
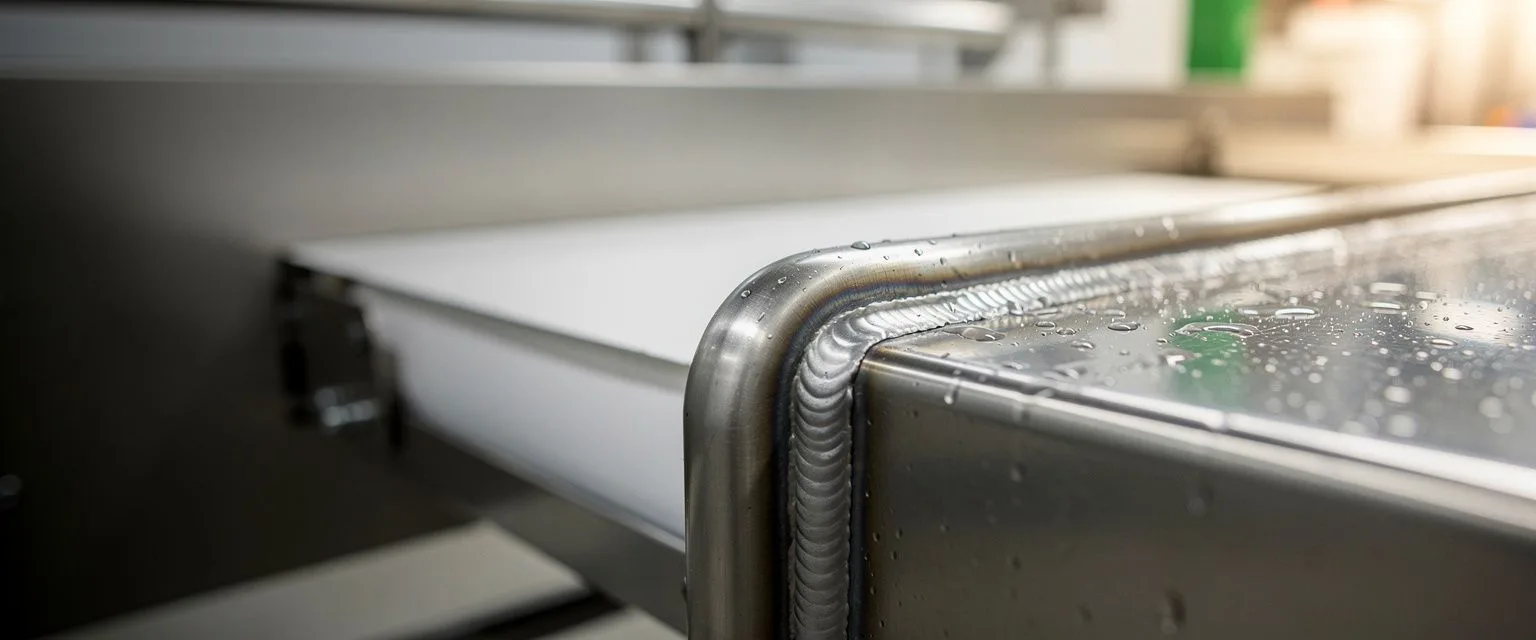
The surface treatment requirements for food contact surfaces focus on reducing bacterial adhesion and facilitating cleaning. A common practice is to polish stainless steel surfaces to Ra 0.8 μm or finer. The lower the roughness, the lower the chance of food residue and microbial growth, and the easier it is to rinse clean during washing. Mechanical polishing is lower in cost and suitable for general filling and forming machines. Electrolytic polishing can further reduce surface roughness and is suitable for continuous egg steaming lines or egg liquid processing equipment that require high hygiene standards. Welded joints must be ground smooth, without grooves or spatter, as these are hard-to-clean areas. Buyers should use a roughness tester to measure actual values during acceptance and inspect the quality of weld seams. The specific level of surface treatment and inspection methods should be confirmed based on the actual product and regulatory requirements.
What are the core principles of hygienic design?
The core principle of hygienic design is to make the machine structure itself effectively cleanable, without relying on the diligence of operators. Specific practices include: avoiding sharp corners and dead zones, using rounded corner designs, using food-grade seals, using sanitary quick-disconnect fittings for pipe connections, and maintaining clearance between the frame and the floor for cleaning. Egg liquid mixing and metering filling equipment, which come into contact with raw egg liquid, carry a high risk of bacteria and require stricter hygienic design. Filling machines, although they contact dough and fillings, still need to avoid residue that could cause cross-contamination. Buyers can request hygienic design documentation from the manufacturer, indicating disassemblable parts, CIP applicability, and recommended cleaning procedures. Even with the correct materials, poorly designed machinery will lose points in hygiene inspections.
What documentation and traceability information should be prepared?
Documentation and traceability information should be prepared starting from the inquiry stage, not just before shipment. Buyers should require the manufacturer to provide: material certificates (indicating stainless steel grade and batch number), CE Declaration of Conformity, food contact material declarations, electrical and pneumatic diagrams, operation manuals, spare parts lists, and risk assessment reports. For plant-wide planning and turnkey projects, factory layout drawings, piping diagrams, and commissioning record formats should also be included. These documents are essential for customs clearance, local factory inspections, and future maintenance. The key to traceability is that every batch of material can be traced back to its source, which serves as the basis for responsibility attribution in the event of a hygiene incident. Document formats and language requirements (English, Thai, etc.) should be agreed upon in the contract in advance. Specific document items and versions should be confirmed based on actual specifications and destination country requirements.
What are the common risks when certifications are insufficient?
Common risks when certifications are insufficient include customs detention, full shipment returns, local fines, and damage to business reputation. In practice, the most frequent situations are: unclear material certificates that lead customs to question the material grade; CE documents missing risk assessments, causing rejection by EU buyers; and surface finishes that do not meet food-grade standards, resulting in a production halt order during local hygiene inspections. Another type of risk is "documents complete but content inconsistent," such as a material certificate stating 304 while 201 stainless steel is actually used, which is easily detected during a factory audit. Buyers should specify acceptance criteria and penalties in the contract and reserve the right to conduct third-party inspections. For first-time suppliers, it is recommended to place a small trial order first to confirm document and quality stability before proceeding with full plant planning. The specific impact of certification risks depends on the destination country's regulations and actual circumstances.
Need an assessment of material and certification configuration based on destination country regulations?
Please provide the destination country, product type, and factory conditions. We will evaluate material grade, surface treatment, and certification document configuration recommendations based on your actual needs, and provide customized quotes for full plant planning and turnkey projects.
延伸主題
- When to Choose 304 vs. 316 Stainless Steel
- Analysis of Differences Between CE and Food Machinery Regulations Across Countries
- Surface Finish Requirements for Food-Contact Surfaces in Food Machinery
- What are the clean design principles for food machinery?
- What Documentation and Traceability Data to Prepare for Food Machinery Exports
- Common Risks of Insufficient Certification